MASS
Annual material use equals mass multiplied by volume. Every gram must serve a demonstrated function.
INDUSTRY · GATED DEVELOPMENT
AQUENORA progresses through tests and stop/go decisions. Each investment authorises the next only when geometry, material, process and performance meet the agreed criteria.
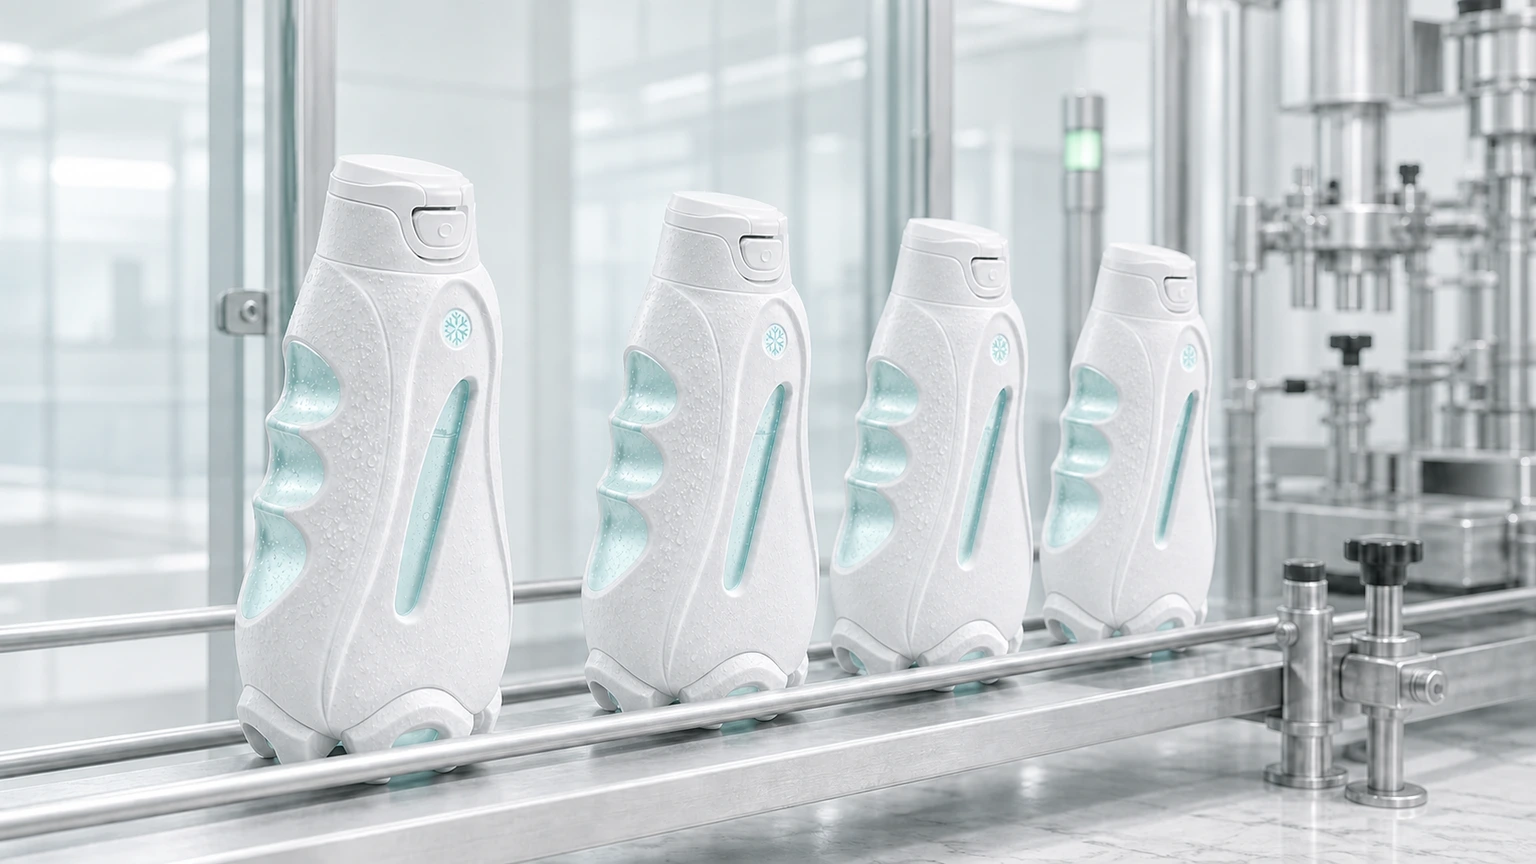
STAGED INVESTMENT
The R2 configuration is a design basis, not mould-ready geometry. The industrial buyer or partner enters before final CAD to align neck standards, equipment, performance, quality control and target cost.
Open the technical dossier ↗INDUSTRIALISATION PLAN
Capacity, shelf life, filling line, logistics, channel and performance are agreed with the industrial buyer or partner.
A purchasable resin is compared with a control solution on a real process.
Form, neck, walls, closure and base become dimensioned, toleranced geometry.
Demoulding, wall distribution, loads, drop behaviour and palletisation are assessed.
Grip, closure, FlowCrown, ThermoSnow and SoftFold are tested separately.
The first near-industrial lot measures variability, scrap and process capability.
Filling, capping, sealing, case, pallet and transport close the DVP&R.
Compliance, specifications, control plan and business case authorise—or stop—the launch.
COST DRIVERS
Unit cost and investment become comparable once geometry, materials and process are frozen and consistent RFQs have been received. Every result must remain traceable to its inputs.
Annual material use equals mass multiplied by volume. Every gram must serve a demonstrated function.
Forming time determines capacity, cavity count and conversion cost.
Real yield enters the cost model before any commercial figure is used.
Closure, indicator and inspection systems must sustain the required production speed.
SUPPLY-CHAIN REQUIREMENTS
Process window, wall distribution, repeatability, vision inspection and scrap.
Top-load, vibration, case, pallet, temperature and transport.
Footprint, stability, display, handling and shelf performance.
Understanding, opening, grip, flow, closing and end of use.
DECISION GATES
Protectable scope and requirements agreed.
ACTIVECAD, tolerances and simulations meet their criteria.
TO BE CLOSEDFunctional prototypes pass the preliminary test plan.
TO BE CLOSEDProcess, quality and cost prove repeatable.
TO BE CLOSEDCompliance, supply and business case are closed.
TO BE CLOSEDNEXT DECISION
The first investment is a focused sprint covering requirements, IP, CAD and DFM. Its output is a documented decision: continue, correct or stop development.
Open the dossier ↗